Fully Automatic Loader is a type of automated equipment that can automatically convey materials to designated machines. Its main purpose is to **reduce manual handling, improve feeding efficiency and improve the working environment**.
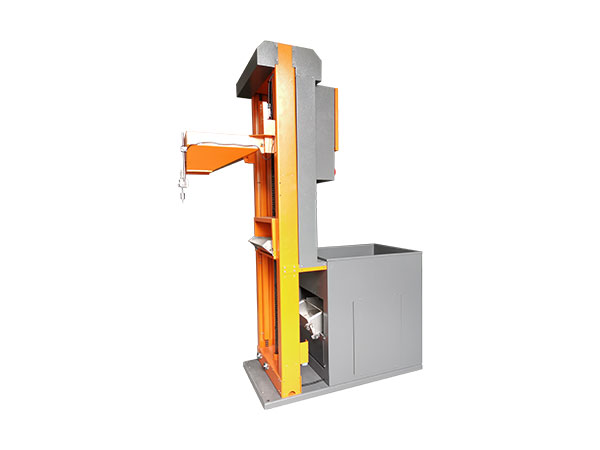
Now let's talk about the common faults of fully automatic loaders.
1. Weak Suction, Unable to Pick Up Material
Symptom: the machine is running, but almost no material comes up into the hopper and suction is very slow.
Causes:
① Air leakage in the piping: the suction hose is cracked, joints are loose, or the sealing ring on the hopper cover is aged and not properly closed; vacuum leaks, resulting in insufficient negative pressure.
② Clogged filter element: powder and returned dust clog the filter element, air cannot be discharged and vacuum cannot build up.
③ The suction gun is inserted too deep and draws in a large amount of air; the material barrel is nearly empty and draws in air.
④ The vacuum pump (vortex air pump) is worn and suction has declined; the pump impeller is dusty.
Countermeasures: check all seals; clean / replace the filter element; adjust the insertion depth of the suction gun; service the air pump.
2. Frequent Suction but the Hopper Never Fills, Repeated Start-Stop
Symptom: the machine keeps starting to suction, but the material level never rises.
Causes:
① The surface of the photoelectric / rotary paddle level sensor is covered with plastic dust, falsely detecting "full" and stopping early.
② The reverse-jet time is set too short, the filter element is not cleaned thoroughly, and resistance grows with each suction.
③ Slight air leakage in the piping, causing intermittent insufficient suction.
3. Loud Noise and Severe Heating of the Vacuum Pump
Symptom: the pump body gets hot with obvious abnormal noise.
Causes:
① The filter element is severely clogged, the air pump load stays too high and it runs overloaded.
② The air pump bearings are worn and the lubricating grease has dried out (can be maintained with a metered grease gun).
③ Dust and foreign objects enter the impeller and scrape the pump casing.
④ Unstable voltage.
Risk: prolonged overheating can burn out the air pump motor.
4. Material Carries a Lot of Dust During Suction, Fine Powder Mixed into the Material
Symptom: more powder appears in the hopper.
Causes: the **filter element is broken and cracked**, so fine powder passes through the filter element and is drawn directly into the hopper;
in severe cases the powder enters the vacuum pump and rapidly wears the impeller.
5. The Machine Does Not Start, Completely Inoperative
Symptom: no response when powered on, no suction.
Causes:
① The emergency stop button has been pressed; power line is broken or the circuit breaker has tripped.
② Control board failure or level sensor failure, causing abnormal signals.
③ A protection alarm is triggered (overload, material shortage alarm lockout).
6. The Loader Does Not Stop, Suction Continues
Symptom: the hopper is already full but the machine keeps suctioning and material overflows.
Causes:
① The level sensor is damaged or displaced; dust coverage prevents it from recognizing a full hopper.
② The sensor wiring has come loose.
③ PLC / control board program failure.
7. Piping Blockage, Material Stuck in the Middle of the Pipe
Symptom: occasionally a little material can be sucked, with frequent material interruptions.
Causes: material caking and long strip-shaped material ends entering the piping; the hose is bent and flattened; conveying distance is too long or there are too many elbows.
8. Frequent Alarms
1. **Material Shortage Alarm**: the material barrel is empty; the suction pipe is blocked; air leakage in the piping; the suction gun is out of the material.
2. **Overload Alarm**: the air pump is jammed; abnormal voltage; the filter element is completely clogged, causing excessive load.
9. Reverse-Jet Function Failure
Symptom: the filter element clogs quickly and there is no automatic dust cleaning action.
Causes: the solenoid valve is damaged; insufficient compressed air pressure; the air pipe has come off; the reverse-jet parameters on the control board are set incorrectly.



 Chinese Version
 English version